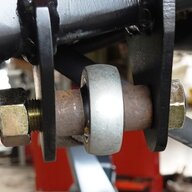
Alright, so here's today's official progress report. Making the mounting brackets for the cross-member was pretty straightforward, so no pictures. I drilled the holes first in one big strip of steel, then cut them off to length and rounded the ends. Then I mounted the cross-member above the skid plate with some .010" shim stock between the cross-member and the skid. I did this to attempt to ensure that 100% of the weight of the transmission mount was on the cross-member once the brackets are welded to the frame. Then, I lined everything up and welded the outsides completely, and heavily tacked the top and bottom on the insides. I let it cool back to ambient temperature, removed the skid and cross-member, and welded the insides. Here's a close-up of one side after reinstalling for a picture:
View attachment 568477
I didn't have the right length bolts, so that's actually a cut piece of the original all-thread that came with the Atlas for the twin stick linkages. Proper Grade 8 bolts will be on their way tomorrow.
And here's the plot twist I teased before dinner. When I was removing the skid, I was getting fine aluminum flakes falling as I loosened the flat-head bolts holding the skid plate on. Thinking that was odd, I investigated. Looking at the countersunk holes, I could see a very sharp witness mark at the top of the taper (the widest part, at the bottom surface of the skid when installed). Right away, I thought, "that meathead machinist put an 82° countersink on this skid!" I was very explicit about it requiring a 90°. However, as it turns out, measure the included angle of a countersunk hole is not so easy!
To confirm, I painted one of the tapers with blue Dykem and tightened it to see what contact I had in the taper. That's the photo in my teaser post above, and if you look closely, you can see that the only contact, where the Dykem is rubbed away, is a very fine line at the widest part of the head, corresponding to the witness mark I was seeing in the skid's hole:
View attachment 568479
Crap - now what?
Mr. Blaine and I had been conversing via email right before this, so I mentioned my issue in an email. A short time later, he called me, and we discussed possible solutions. He came up with the best one (not surprising at all), as he said, "I just thought of the best solution, but you're not going to like it." I groaned, and he said, "you can drill out the M12-1.75 nutserts and replace them with the earlier 1/2-13 nutserts because the 1/2-13 flatheads have an 82° countersink." He's right, I don't like it - installing those huge nutserts is a special kind of fun. However, he's also right that it's the best solution.
So, now, before I can put this back together, I'll be drilling out 14 metric nutserts and replacing them with SAE. Fun! Stay tuned...






 I then turned my attention back to the tub mods. Until I looked, I didn't realize how many spot welds between the two layers of the tub there were right in the area where I used the ram. I should have paid much more attention! If I did, I don't believe I'd have kinked the floor because I'd have cut the welds first. If you're reading this because you're getting ready to do a similar tummy tuck/Atlas 4-speed installation, mind those spot welds! There are eleven welds in an area about 5" x 8" that I cut this afternoon (the upper right rectangle below), including two that hold the right front seat bolt boss to the floor for the driver-side seat (removed before the picture:
 I was hoping to avoid welding and/or grinding inside the cab, but I think I'm going to have to in order to fix some of the ugliness. I'll have to bag the dash and cover everything - fun!
 Here's the piece in place:


