
You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
Which welding wire for outboarding shocks?
- Thread starter astjp2
- Start date

I have to admit that i am about the same spot except still prefer to weld with acetylene. Built my first two go-kart racing cages that way and still prefer handling a torch vs stick or MIG.Globular Transfer.
I’m an old school 7018 low hydrogen guy at heart, but had to learn to embrace mig/tig when all the fabricators were making the switch years ago.
Last edited:
is this one of the models with the "remote" fine tune control? You would basically yank the fine tune out of the face of the machine and it would take an standard extension cord that would plug into the fine tune and machine and you could have the fine tune next to you while you were welding. Hobart was ahead of their time.Speaking of old school, this was in my Granfathers shop, then my dads shop and I have had it in my shop for 20yrs. Really pure DC output, touch the stick and it starts to burn. 220v single phase too. It burned up on start up a few years ago. I had intended to restore it and get a new transformer but I decided to give it to a friend who has a 60's garage in AZ. He is retired and will take the time to restore it properly.
That's 3 of us who know what spray arc transfer is, just need the other 2 now.The "2" in 98/2 is usually oxygen. That said, it is best used to stabilize spray arc. Shortarc transfer is best with a 75/25 (argon and c02). Spraying is mostly a flat position mode.
The OP asked about what type, not sure if anyone mentioned the type of wire?? The best all around wire spec for that machine (nice machine BTW) and fixing Jeeps is Lincoln L56 wire. It has a spec of E70S-6. All position medium freezing, low carbon and low silica composition.
My shop is plumbed with gas that we mix ourselves, We hook a 230l liquid argon dewar and a T (330cu feet??) HP oxy bottle to a Thermco mixer. We generally run 2.5% oxy unless it is some crappy porosity and sand filled chinese material. We run a true spray at 430a and 32v It is beautiful to watch. We have a trailing argon plate to protect the molten puddle from air attack. Material has to be flat or very close, much of an angle and the weld flows like water.
View attachment 224890

Old school here too. Not as often as I once did but I still weld sheet metal with an O/A torch and no rod from time to time.Globular Transfer
I’m an old school 7018 low hydrogen guy at heart, but had to learn to embrace mig/tig when all the fabricators were making the switch years ago.
My new welder can do it. That’s the extent of my knowledgeThat's 3 of us who know what spray arc transfer is, just need the other 2 now.

My new welder can do it. That’s the extent of my knowledge
I've watched a few YouTube videos over the years. I knew what spray arc transfer was before today.
I can’t find the spray button on mine...That's 3 of us who know what spray arc transfer is, just need the other 2 now.

Yeah all to often people think that bigger is better but for welding the opposite is more often true. I had to fill pin holes in the floor of an XJ and the only welder I had available to me at the time was a Millermatic 210 running 045 wire. Talk about bringing a cannon to a gun fight.I suck at welding coped tube joints so I run some .030 so I don't have to weld quite so fast. Just enough of a band-aid to not look worse than normal.
Haha, ya, I just went from .030 to .035 cause I could not get the 030 to feed without birdnesting after the last pair of rolls. I am not a small wire dia guy. My shop uses about 800lbs a week of .0625" wire. It frustrates me to use tiny wire.Yeah all to often people think that bigger is better but for welding the opposite is more often true. I had to fill pin holes in the floor of an XJ and the only welder I had available to me at the time was a Millermatic 210 running 045 wire. Talk about bringing a cannon to a gun fight.
This is my personal garage welder. It (now) runs 035 on one side and 045 on the other. The power source is a XMT 456. Love the invertor size. runs clean and is easy on power use.
My shop has four of these, these guys are animals:

OP, sorry to derail. In an attempt to get back on track, outboard done with E70-S6 .045" wire:
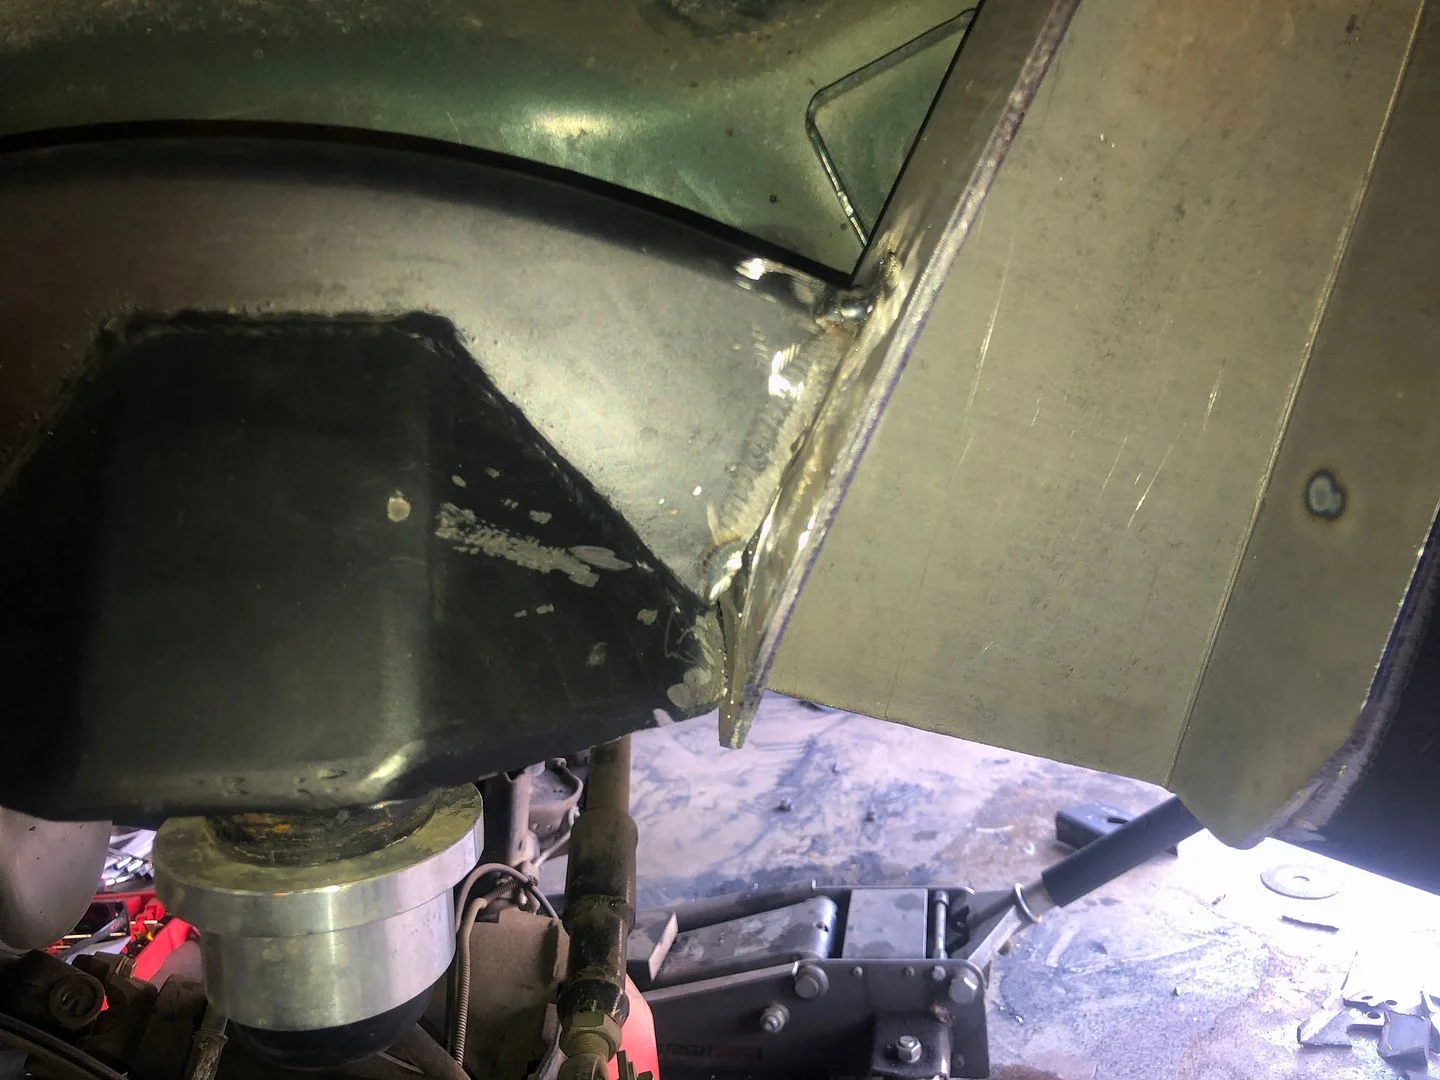

Fit check before weld (cycle, cycle, cycle again, etc..)
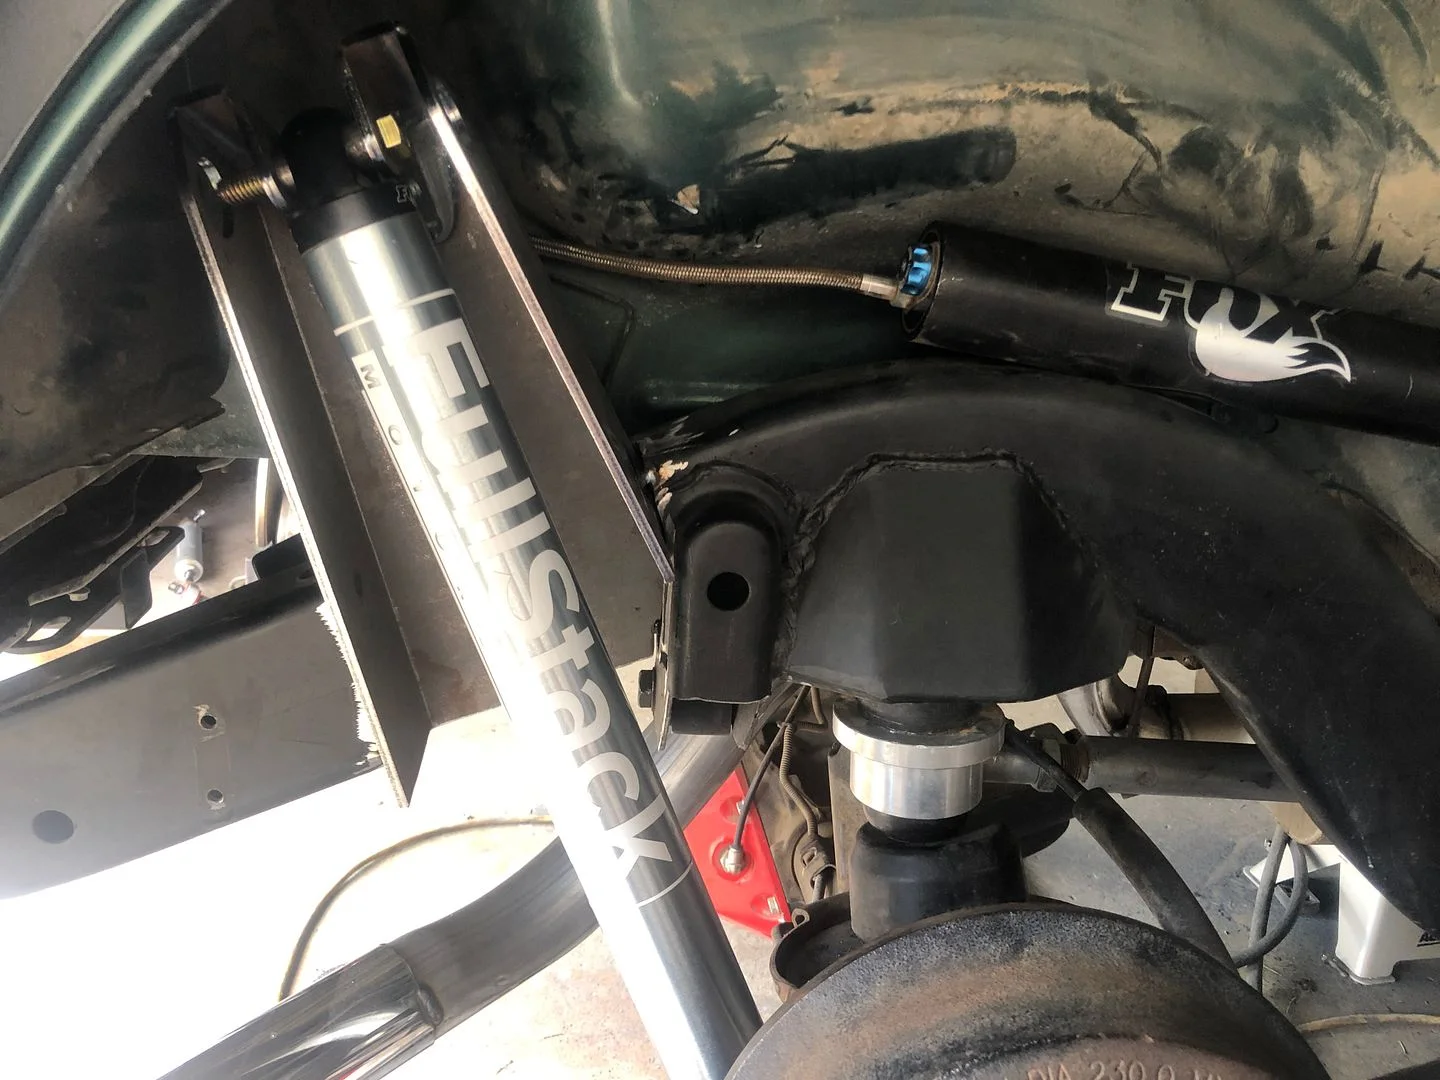
DON'T do this:
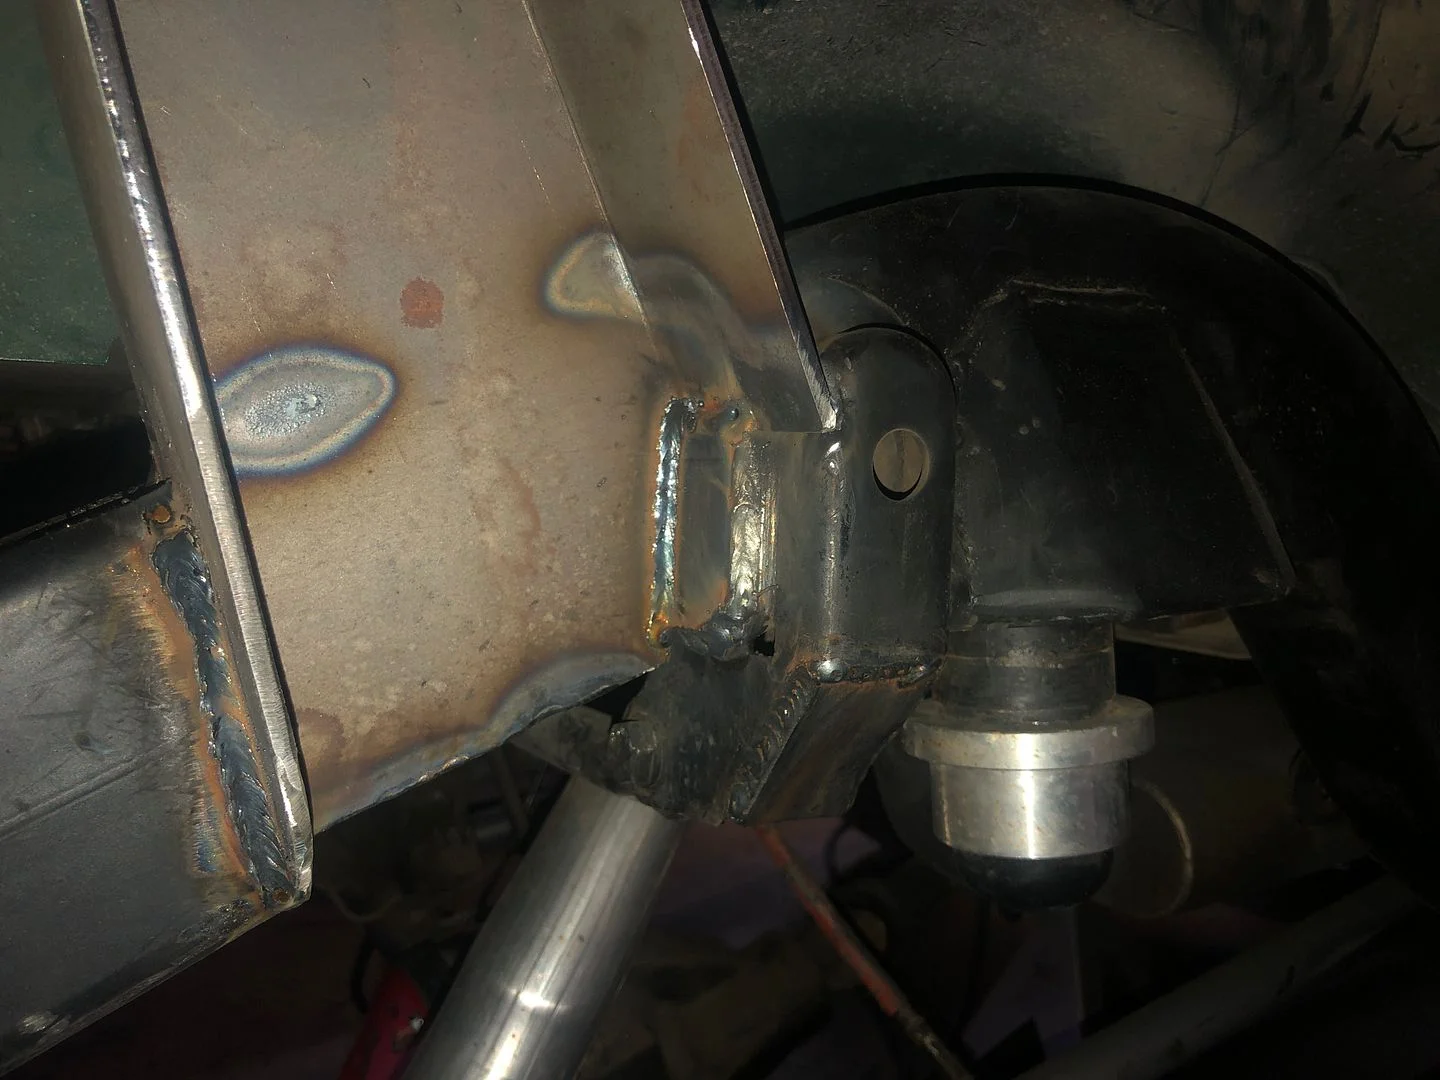
Make a new trackbar mount, avoid the extra work. MrBlaines advice came too late to help me, and it would have been easier and mo betta.
Fit check before weld (cycle, cycle, cycle again, etc..)
DON'T do this:
Make a new trackbar mount, avoid the extra work. MrBlaines advice came too late to help me, and it would have been easier and mo betta.
Fughuert
TJ Enthusiast
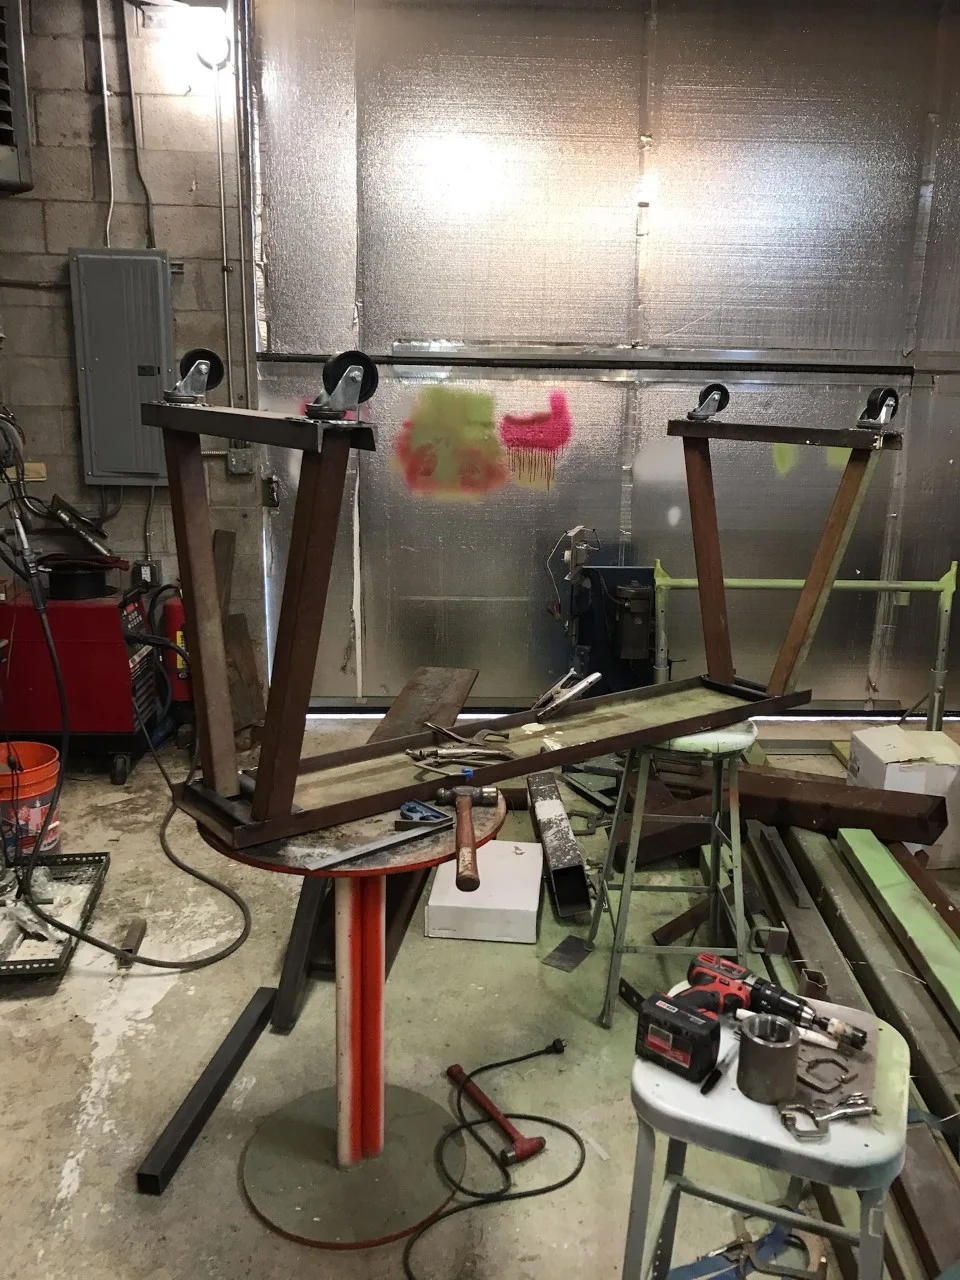
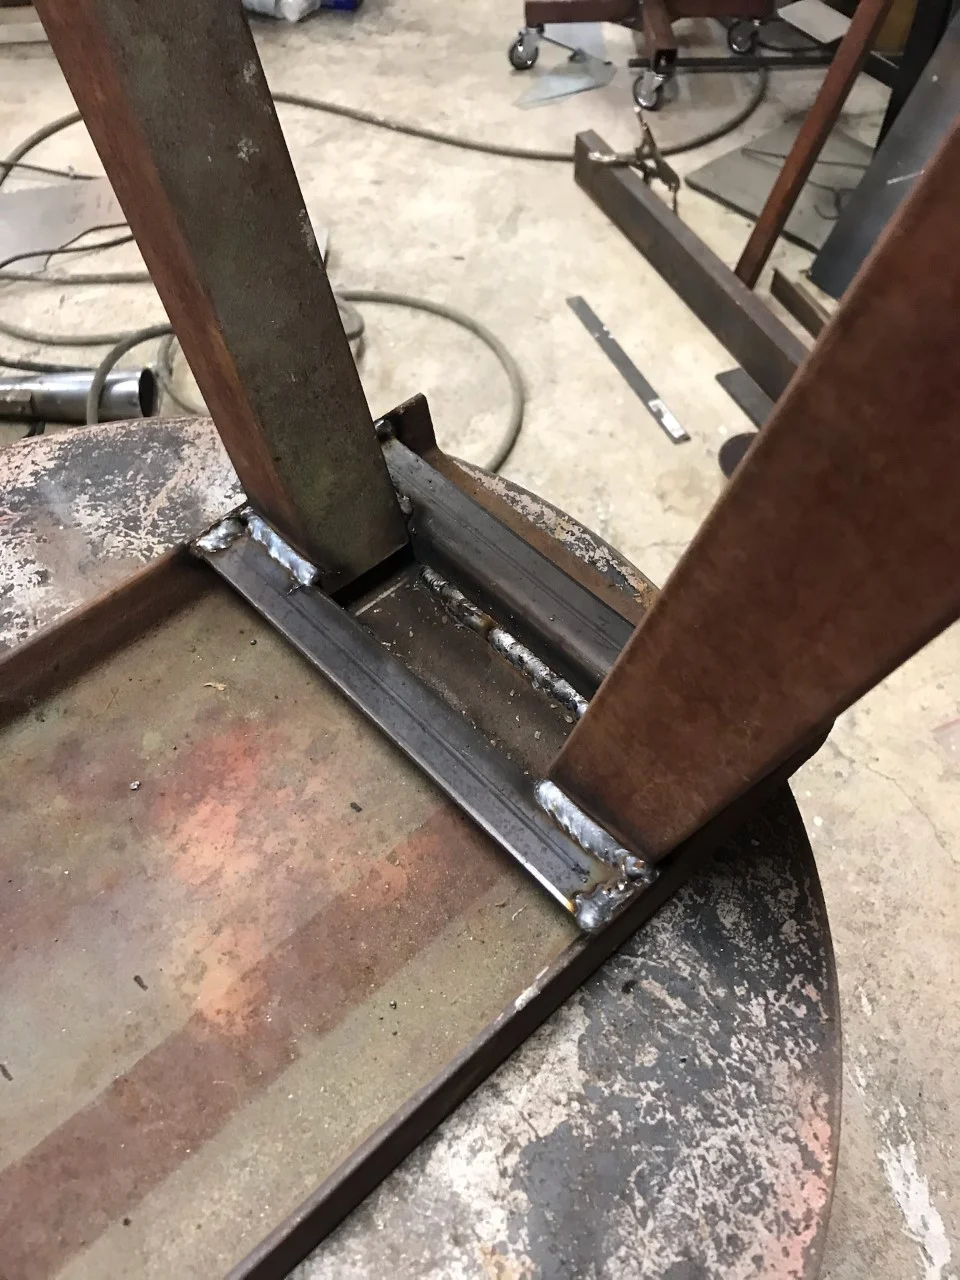
So when I pulled out the old spool this weekend, I found it was Hobart ER70s3, the new spool of s6 worked better on the rusty metal I was welding. Building a table to put some machines on. Tim
Similar threads


- Replies
- 63
- Views
- 17,320


- Replies
- 13
- Views
- 2,842


- Replies
- 4
- Views
- 840


- Replies
- 12
- Views
- 1,680
